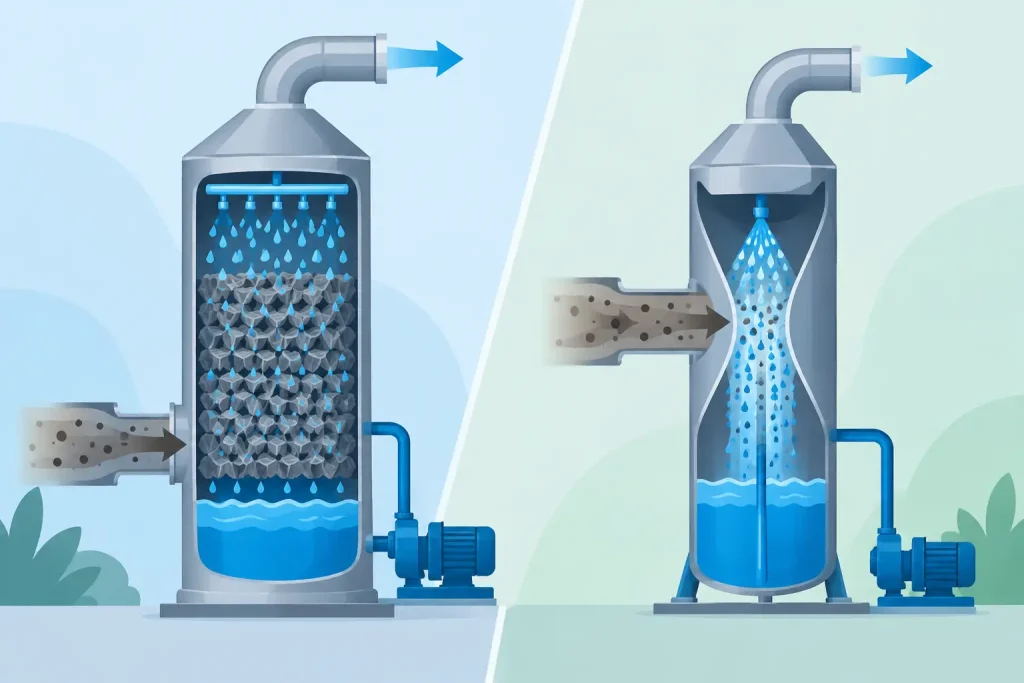
A packed scrubber versus venturi scrubber decision is rarely settled by collection efficiency alone. The right unit must control the actual contaminant, remain stable through production changes, fit available fan capacity, and produce operating records that support permit compliance. For plant managers and EHS leaders, the consequence of choosing incorrectly is not merely higher utility cost. It can mean recurring exceedances, unplanned shutdowns, corrosion damage, and difficult conversations during inspections.
Both technologies use liquid to remove contaminants from an exhaust stream, but they create gas-liquid contact in fundamentally different ways. A packed tower relies on surface area and residence time. A venturi scrubber relies on high-energy atomization and intense turbulence. That difference determines where each system performs best.
Packed Scrubber Versus Venturi Scrubber: The Core Difference
A packed scrubber, often called a packed tower scrubber, directs contaminated gas through a vessel containing structured or random packing. Scrubbing liquid is distributed over the packing, creating a wetted surface across which contaminants transfer from the gas phase into the liquid. The gas commonly flows upward while liquid flows downward, although configuration depends on the duty.
This design is particularly effective for gaseous pollutants that must be absorbed or neutralized, including acid gases, alkaline gases, odor compounds, and certain soluble VOCs. With the correct reagent and pH control, a packed tower provides substantial contact area without requiring extreme gas velocity.
A venturi scrubber accelerates gas through a constricted throat. Liquid introduced at or near the throat is sheared into fine droplets by the high-velocity gas stream. Particles collide with these droplets and are captured, after which a downstream separator removes liquid droplets from the cleaned gas.
The venturi mechanism makes it well suited to fine particulate matter, sticky dusts, metal fumes, and high-temperature particulate-laden streams where conventional dry filtration may face limitations. Its strength is energetic particle capture, not extended gas absorption.
Contaminant Characteristics Should Lead the Specification
The first engineering question is not which scrubber is generally better. It is whether the emission is primarily gas, particulate, or a mixed stream.
For a gas-phase duty, such as hydrochloric acid mist, ammonia, sulfur compounds, or odor-bearing process exhaust, a packed scrubber is generally the more appropriate starting point. Absorption depends on solubility, chemical reaction rate, liquid-to-gas ratio, packing depth, distribution quality, and recirculating liquor chemistry. Selecting the wrong reagent, allowing pH to drift, or using poor liquid distribution can reduce removal performance even when the tower itself appears mechanically sound.
For submicron to coarse particulate matter, a venturi scrubber can deliver high collection efficiency when designed at the required pressure drop. It is commonly considered for foundry fumes, metallurgical applications, pigment or mineral dust, and other difficult particulate services. The trade-off is energy. Fine-particle collection requires higher throat velocity, and that velocity must be supplied by the induced-draft fan.
Mixed emissions require closer assessment. A process may release acid mist together with dust, or fume together with a soluble gas. In these cases, a staged arrangement can be more defensible than asking one device to perform incompatible duties. A venturi section may first remove particulate, followed by a packed tower for absorption, with a properly designed mist eliminator protecting the stack discharge. The final arrangement should be based on representative gas analysis, mass loading, temperature, moisture content, and required outlet limits.
Pressure Drop Is an Operating-Cost Decision
Pressure drop is one of the clearest differences between the two systems. A packed tower normally operates at a lower pressure drop than a high-energy venturi scrubber. This can reduce fan horsepower and ongoing electrical consumption, provided the packing remains clean and the liquid distribution system performs as designed.
A venturi scrubber deliberately creates a substantial pressure loss to generate the turbulence and droplet atomization needed for particulate capture. Higher pressure drop generally supports improved fine-particle removal, but it also raises fan energy demand. Specifying a venturi without checking available static pressure, fan curve, motor margin, and duct condition can result in poor capture at the hood or inadequate throughput at the process.
This is why a scrubber should not be evaluated as an isolated vessel. The complete system includes hoods, ducts, dampers, fans, pumps, mist eliminators, stack geometry, and controls. A field audit should verify capture velocity and duct transport conditions before a replacement or upgrade is approved. Strong outlet performance at the scrubber has limited value if contaminants are escaping into the work area before they enter the duct.
Water, Chemistry, and Wastewater Need Equal Attention
Wet scrubbers transfer contaminants from air into liquid. They do not eliminate the need to manage the captured material. Both packed and venturi scrubbers require a defined approach for makeup water, blowdown, sludge handling, pH adjustment, chemical storage, and wastewater treatment or authorized disposal.
A packed scrubber often relies on chemical control as part of its removal mechanism. Acid gas absorption may require caustic dosing, while alkaline gas treatment may require an acidic reagent. Operators should track pH, conductivity where relevant, recirculation flow, tank level, and chemical consumption. A sudden increase in dosing demand can indicate a process change, excessive inlet loading, or a control problem.
Venturi scrubbers can generate solids-laden recirculating liquor. In applications with high dust loading, solids buildup may block nozzles, erode pumps, reduce throat performance, and overload mist eliminators. Settling tanks, hydrocyclones, filtration, or controlled blowdown may be necessary depending on particle characteristics.
Water availability also matters. A closed-loop system reduces fresh-water demand, but recirculation concentrates dissolved salts and captured contaminants. The system must maintain a practical balance between water conservation, corrosion control, scaling risk, and wastewater compliance.
Maintenance Requirements Are Different, Not Optional
Packed towers require attention to the packing bed, liquid distributors, spray nozzles, pumps, demisters, vessel lining, and chemical feed equipment. Poor distribution can create dry zones and channeling, where gas bypasses the intended contact area. Scaling, biological growth, or solids deposition can increase pressure drop and reduce absorption efficiency. Demister fouling may cause liquid carryover, visible plume, or downstream corrosion.
Venturi scrubbers require inspection of the throat, liquid injection points, pumps, separators, and slurry-handling components. Abrasive dust can wear the venturi throat and elbows. Sticky material may accumulate in the separator or demister. Because performance is closely tied to pressure drop and liquid flow, instrumentation should be treated as part of the control system rather than an accessory.
For either technology, the operating log should document differential pressure, recirculation flow, pump status, tank level, pH where applicable, and visible stack conditions. Trend data is more useful than occasional readings. A gradual shift in pressure drop or chemical use often identifies a developing problem before it becomes a failed compliance test.
How to Select the Right Scrubber
A reliable selection process begins with data collection. Engineers should establish exhaust volume across normal and peak production, pollutant composition, particle-size distribution, inlet temperature, moisture, gas chemistry, contaminant loading, required outlet concentration, and available utilities. If the existing system is underperforming, stack sampling and field measurements should distinguish between poor capture, inadequate airflow, insufficient treatment capacity, or an operational control issue.
A packed scrubber is usually favored when the duty is gas absorption or chemical neutralization and moderate pressure drop is preferred. A venturi scrubber is often favored when high-efficiency particulate collection is needed for difficult dust or fume, and the facility can support higher fan energy and slurry management requirements.
Material selection deserves early review. Corrosive gas streams may require FRP, polypropylene, PVC, rubber-lined steel, stainless steel, or specialized linings. Temperature, chemical concentration, chloride exposure, and cleaning practices all affect the correct choice. The lowest initial equipment price can become expensive if materials are not matched to the process environment.
Compliance Requires Proof of Performance
Compliance-oriented projects should define acceptance criteria before fabrication. These may include airflow, pressure drop, liquid circulation rate, pH range, fan static pressure, stack concentration, and capture performance at the source. Testing and commissioning should confirm that equipment is operating at its design point, not simply that motors are running.
For facilities subject to air permits, occupational exposure requirements, or customer environmental audits, retain commissioning records, calibration documentation, maintenance history, chemical logs, and stack sampling reports. Where continuous or online monitoring is appropriate, trend alarms can help maintenance teams respond before a deviation becomes an emissions event.
Master Jaya Group approaches wet-scrubber projects as lifecycle emission-control systems, combining engineering design, fabrication, installation, testing and commissioning, field auditing, stack sampling, and after-sales servicing. That level of accountability is particularly valuable where a scrubber upgrade must improve both plant reliability and defensible compliance documentation.
The practical choice is to match the scrubber to the contaminant and then verify that the entire air-handling system can sustain its design conditions. A well-engineered packed tower or venturi scrubber becomes a dependable compliance asset only when operators can measure, maintain, and prove its performance over time.