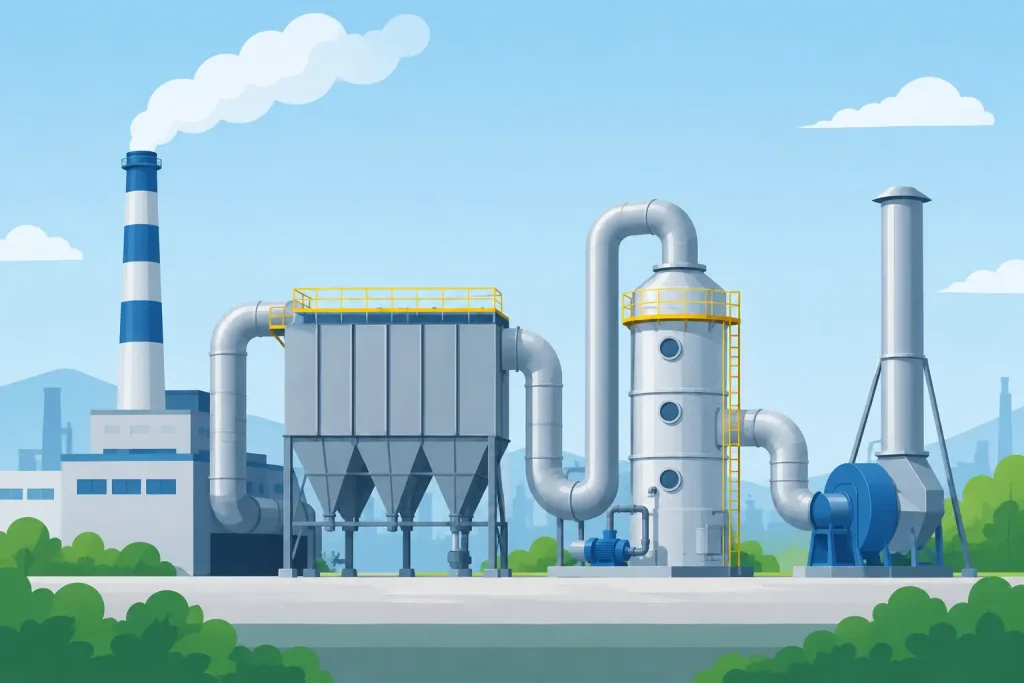
A collector that captures dust at the pickup point but loses airflow across a clogged filter is not a pollution-control solution. It is an operational risk. Selecting the top pollution control equipment for an industrial plant starts with the actual emission source, contaminant properties, required outlet performance, and the documentation needed to defend compliance during an audit or inspection.
For plant managers, EHS leaders, and project engineers, the objective is not simply to install a device at the end of a duct. The objective is sustained control: stable suction at hoods, acceptable stack emissions, safe maintenance access, reliable spare parts, and verified performance after commissioning. The right technology depends on whether the facility is managing particulate, acid gas, oil mist, odor, volatile organic compounds (VOCs), or combustion-related emissions.
Top Pollution Control Equipment by Contaminant
Pulse-jet dust collectors for dry particulate
Pulse-jet dust collectors are widely used where processes generate dry dust, including metal grinding, casting, cutting, powder handling, bagging, food processing, animal feed production, and bulk material transfer. Contaminated air enters the collector, where filter bags or cartridges retain particulate. Timed or differential-pressure-controlled compressed-air pulses clean the filter media and discharge collected dust into a hopper.
Their principal advantage is high particulate collection efficiency with continuous operation. A properly engineered system can maintain strong capture at the source while keeping pressure drop within the design range. This makes pulse-jet collectors a practical choice where production cannot stop for frequent manual filter cleaning.
The trade-off is that filter selection and dust characteristics matter greatly. Fine, sticky, hygroscopic, oily, combustible, or high-temperature dust may require specialized media, pre-separation, explosion protection, insulation, or temperature control. A collector should never be sized only by fan airflow. Hood design, duct transport velocity, air-to-cloth ratio, dust loading, compressed-air quality, and discharge arrangements all affect final performance.
Cyclones and multi-cyclones for coarse dust and pre-separation
Cyclones use centrifugal force to separate heavier particles from an airstream. They have no filter bags, operate at elevated temperatures, and have relatively simple mechanical construction. Multi-cyclones use multiple small cyclone tubes to improve collection of smaller particles compared with a single large cyclone.
These units are often effective as primary separators for coarse dust, sparks, abrasive particles, boiler fly ash, or high-loading process streams. They can also protect downstream equipment by reducing particulate loading before a baghouse, wet scrubber, or electrostatic precipitator.
Cyclones are not usually the final answer when stringent fine-particulate limits apply. Their efficiency declines as particles become smaller, so a cyclone-only system may not provide the outlet result required by a permit or internal air-quality target. Their value is often in a staged system, where durable pre-separation improves the reliability of the final control device.
Packed tower scrubbers for gases, fumes, and soluble pollutants
Packed tower scrubbers bring contaminated gas into close contact with a recirculating liquid across packing media. They are commonly applied to acid gases, alkaline fumes, ammonia, odor-causing compounds, and process emissions that can be absorbed or neutralized by a selected scrubbing solution.
A packed tower is not a generic wet treatment solution. Chemical compatibility, inlet concentration, gas temperature, liquid-to-gas ratio, packing type, circulation rate, reagent consumption, pH control, and mist elimination must be engineered together. For example, an acidic gas may require an alkaline reagent, while alkaline emissions may require acidic treatment. The spent liquor and blowdown also require responsible handling under applicable wastewater requirements.
Wet scrubbers can be especially suitable where a process stream is hot, moist, or carries a gas contaminant that is difficult to manage with dry filtration. However, they introduce pumps, nozzles, corrosion considerations, water use, and chemical-management duties. Routine inspection of packing condition, recirculation pumps, pH instruments, and mist eliminators is essential to prevent declining removal efficiency.
Electrostatic precipitators for fine particulate at high flow
Electrostatic precipitators, or ESPs, electrically charge particulate and collect it on oppositely charged plates. They are frequently considered for large gas volumes, elevated temperatures, and fine particulate applications, particularly in thermal and combustion-related processes.
An ESP can offer low pressure drop compared with certain filtration systems and can handle substantial flow rates. Yet its performance is sensitive to dust resistivity, gas composition, temperature, electrical field conditions, plate-cleaning performance, and gas distribution. It is a specialized system that requires disciplined operation and maintenance rather than a fit-and-forget installation.
Where process conditions vary substantially, a feasibility review should assess particulate properties across the full operating range. The best design point on paper is of limited value if the unit loses effectiveness during startup, load changes, or fuel variation.
Regenerative thermal oxidizers for VOC destruction
Regenerative thermal oxidizers (RTOs) destroy VOCs and certain odor compounds through high-temperature oxidation. Ceramic heat-recovery beds reduce fuel demand by transferring heat from treated exhaust to incoming process air, making RTOs appropriate for continuous VOC streams where destruction efficiency and energy recovery are priorities.
RTO selection requires a close review of VOC concentration, flow variability, moisture, halogenated compounds, sulfur, silicone contamination, particulate loading, and the possibility of heat recovery or autothermal operation. Some streams require upstream filtration or conditioning to protect ceramic media and switching valves. Others may create secondary pollutants or corrosive byproducts that demand additional treatment.
The capital and fuel requirements can be substantial, but an RTO may be justified when a plant must control significant VOC emissions with dependable destruction performance. The decision should consider total lifecycle cost, including burners, controls, refractory, valve maintenance, and emissions monitoring, not only the purchase price.
Activated carbon filters for adsorption and odor control
Activated carbon filters remove selected VOCs, odors, and solvent vapors through adsorption. They are often used for lower-flow applications, polishing duties, intermittent emissions, or streams that are unsuitable for direct thermal oxidation.
Carbon performance depends on contaminant type, concentration, humidity, temperature, contact time, and bed depth. Breakthrough can occur before an odor is obvious, which makes scheduled sampling, bed monitoring, or a defined change-out plan important. Carbon is not a universal answer for high-concentration, high-moisture, or poorly characterized streams.
Facilities should also evaluate fire risk, heat generation, disposal requirements for spent media, and whether a lead-lag vessel arrangement is needed to maintain control during carbon replacement.
Air strippers for volatile contaminants in water
Air strippers address volatile contaminants in water by transferring them from the liquid phase into an air stream. They may be relevant where industrial wastewater, groundwater, or process water contains volatile compounds that must be removed before reuse or further treatment.
The stripped air cannot be ignored. It may require activated carbon adsorption, thermal oxidation, or another air-pollution control step. A complete design therefore evaluates both water-treatment performance and the fate of the resulting off-gas.
How to Select Pollution Control Equipment That Performs
The first step is source characterization. Identify the emission point, flow rate, temperature, moisture, oxygen content, particulate size distribution, gas chemistry, concentration range, and operating hours. Stack sampling, field auditing, and process review provide a far more defensible basis for design than assumptions based on equipment nameplate capacity.
Next, define the compliance target. This may include permit conditions, local air regulations, occupational exposure requirements, stack-emission limits, and internal ESG objectives. Facilities operating under Malaysia’s Clean Air Regulations 2014 or DOSH local exhaust ventilation requirements, for example, need designs and records that address those specific obligations. US facilities should align the design with applicable federal, state, and local permit requirements. The governing limit, test method, and reporting expectation should be clear before equipment is fabricated.
Capture is as important as filtration or treatment. A high-efficiency collector cannot compensate for a poorly located hood, undersized ductwork, excessive elbows, air leakage, or an incorrectly selected fan. For worker-exposure control, local exhaust ventilation must pull contaminants away from the breathing zone at a velocity appropriate to the process without disrupting production.
Finally, evaluate maintainability. Confirm access for filter replacement, hopper discharge, pump servicing, washdown, carbon change-out, and safe isolation. Specify differential-pressure gauges, airflow indicators, pH instruments, temperature alarms, and interlocks where needed. Online performance monitoring can give operations teams early warning of declining suction, abnormal pressure drop, or equipment downtime before an issue becomes a failed test result.
Engineering, Commissioning, and Lifecycle Support
The strongest pollution-control projects connect design to accountability. That includes engineering calculations, fabrication quality, installation supervision, testing and commissioning, baseline performance verification, operating procedures, preventive maintenance, and spare-parts readiness. An ISO 9001:2015-certified provider with in-house fabrication capability can help reduce the handoffs that often create gaps between design intent and site performance.
Master Jaya Group approaches these projects as a full-lifecycle responsibility, from field auditing and system design through stack sampling, commissioning, servicing, upgrades, and compliance-focused monitoring. Training for responsible personnel, including CePSO and CePBFO competency pathways where relevant, further supports consistent operation after handover.
Before approving a system, ask one practical question: can your team demonstrate, six months after startup, that it is still capturing, treating, and documenting emissions as designed? Equipment selection becomes much clearer when the answer must be supported by operating data, maintenance records, and verified field performance.